Three hundred millimetres is a category decision disguised as a dimension
The step from a two hundred to a three hundred millimetre span is usually presented as a tolerance improvement. It is actually a decision about which product categories the line will carry, and the categories it excludes are the ones that generate the manual lane.
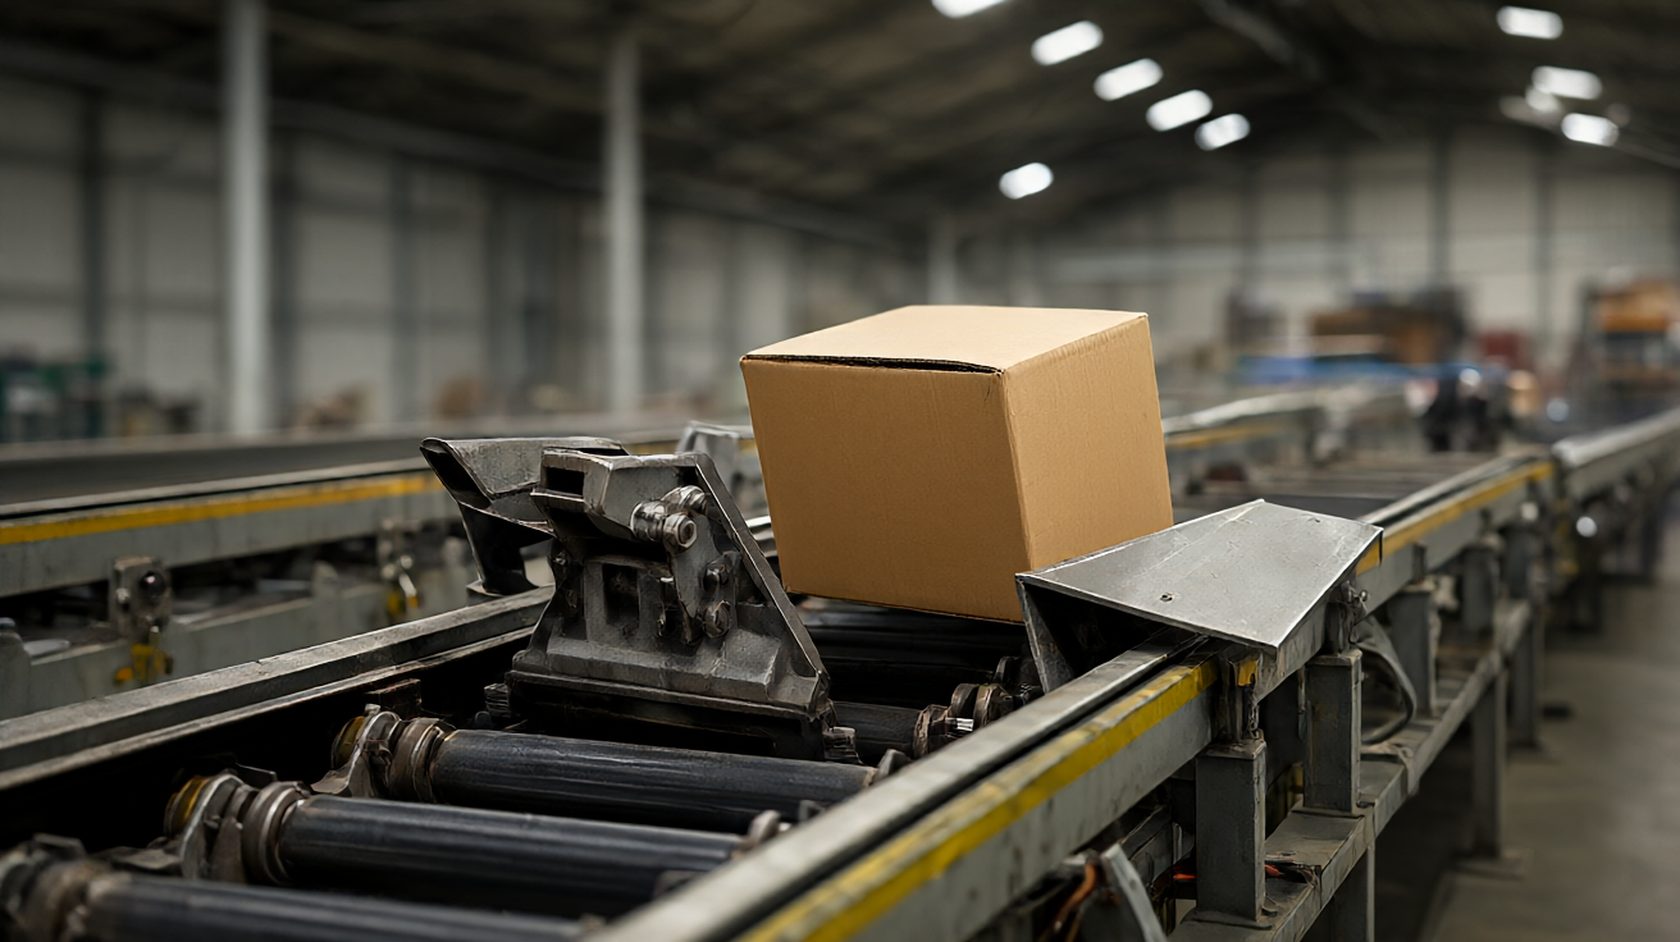
What the extra span actually admits
The step admits the retail carton. A shoe box standing on its base, a small appliance box, a boxed toy, a gift set, a two pack of anything. These are not exotic shapes, they are the standard output of consumer packaging, and they are the shapes a two hundred millimetre span refuses.
It also admits the bag that has settled into a non rectangular shape. A poly mailer with a garment inside is wider at the middle than at the ends, and a span that was specified from the flat dimensions of the mailer will still fail once the garment is inside it.
What it does not admit is the large format carton, the furniture box, the appliance that ships in its own retail packaging at three hundred and fifty millimetres or more. Those remain outside, and the point of the decision is to know how large that outside population is before the line is ordered.
So the specification work is a category census rather than a dimension measurement. List the categories, measure the packed width of each, sort by volume, and find the point on the list where the cumulative share reaches the target. That point is the width the line needs.
Single lane and dual lane are different purchases
A three hundred millimetre span can carry one retail carton comfortably or two narrow parcels abreast. Those are two different operating modes, and the second one is a system capability rather than a belt capability.
Dual lane requires the induction to place two parcels within the same segment, the divert to reach both positions, and the chutes to be arranged so that two parcels of different destinations can leave in the same pass. Each of those is a separate engineering question.
Most installations that claim dual lane operation use it as a peak mode rather than a design assumption, because the destinations rarely align. Two parcels travelling abreast that need different chutes require two passes, and the second pass costs the same capacity as if they had travelled singly.
The honest specification therefore states the primary mode and the exception mode separately, with the throughput of each. A line quoted at a single throughput figure that assumes dual lane is quoting the exception mode, and the buyer will operate in the primary mode most of the time.
The shoe box has two orientations and they perform differently
A shoe box on its base occupies the shorter dimension across the belt and the longer dimension along it. A shoe box on its side does the opposite. Which orientation the induction produces is usually a matter of how the parcel arrives from upstream, not a decision anyone made.
The on base orientation is stable and travels well. The on side orientation has a higher centre of gravity and a smaller contact patch, so it drifts and it rotates at the first lateral force. On a narrow belt with a centring device, the on side box is the one that ends up against a guard.
The orientation also changes the pitch consumed. An on side box may be longer along the belt than an on base box of the same product, which means the same parcel consumes different capacity depending on how it happens to be placed.
The control is an orientation gate or a manual standard at the induction. Neither is expensive, and both are cheaper than the jam that an on side box causes at the first divert. The gate is the version that works at volume.
Soft parcels and rigid parcels fail differently
A soft parcel fails by deforming. It spreads under the centring wheels, it sags into a gap, and it changes shape between the infeed measurement and the divert. A rigid parcel fails by catching. It does not deform, so the energy of the contact goes into rotation or into the guard.
The same guard clearance is therefore adequate for one and marginal for the other. A soft parcel that overhangs will usually be pushed back onto the belt. A rigid parcel that overhangs will pivot, and the pivot is what stops the line.
This is the argument for measuring the mix in two groups rather than one. A line specified from an average that blends soft and rigid parcels will be under specified for the rigid tail, and the rigid tail is the one that produces the stoppages.
The countermeasure is usually a guide rather than a wider belt. A guide that keeps rigid parcels centred and lets soft parcels deform against it costs less than the extra span and addresses the failure that matters. It requires the guide to be placed where the parcel is already settled, not at the induction.
Centring has less margin to work with
Centring on a wide belt is forgiving because there is room to be wrong. Centring on a narrow belt has to be accurate, because the correction available is smaller than the error it might have to fix. A device that moves a parcel twenty millimetres is adequate on a wide span and useless on a narrow one.
The centring device therefore has to be selected against the observed spread of parcel positions at the infeed. A spread measured over a week of real inductions is the only number that matters, and it is usually wider than the spread assumed at design.
Two devices in series work better than one device with a larger stroke, because the first removes the gross error and the second removes the residual. The cost is length along the infeed, which is floor space rather than money, and floor space at the infeed is usually available.
The measurement point for whether centring is working is the divert, as with any tracking question. A parcel that leaves the centring device centred and arrives at the divert offset is a tracking problem, and it will not be fixed by adding a third centring device.
Divert geometry is coupled to the span
A divert that pushes a parcel sideways has to move it across the belt within the segment. On a narrow belt the distance is shorter, which means the same divert completes the move in less time and the window requirement is easier to meet.
This is the one place where a narrower belt is genuinely better. The push distance is proportional to the belt width, so a narrow line can run faster or use a slower, gentler divert and still clear the parcel before the segment ends.
The trade appears at the chute. A chute that receives a parcel from a narrow belt has to accept the parcel's long dimension as it arrives sideways, so the chute opening is larger than the belt width. The chute, not the belt, becomes the constraint on parcel size at that destination.
Which means the width decision has to be made together with the chute design rather than before it. A line specified at the belt and then fitted with chutes sized for the belt will reject parcels that the belt could have carried.
Where the cost difference actually sits
The increment is not a belt price. It is frame, guards, centring, divert stroke, chute openings, footprint and the structural allowance for the wider load. Each scales with the span, and the sum is usually a meaningful share of the line cost.
The offsetting saving is the manual lane. Every category the narrow line excludes has to be handled somewhere, and that somewhere has labour, floor space and a separate process. The saving is recurring and the cost is one time, which is the correct way to compare them.
The comparison should be made per parcel rather than per line. Divide the incremental cost by the number of parcels the wider span allows the line to carry over its life, and compare that to the labour cost per parcel in the manual lane. The result is usually decisive in one direction.
The other saving is jam recovery. A line that jams regularly has a labour cost that appears as downtime rather than as a line item, and it is invisible in the purchase comparison. The narrow line that jams is cheaper on paper and more expensive in operation.
Why not simply go wider
The next span up carries more and costs more, and the reason not to take it is that the extra capacity is unused. A line sized for a parcel population that does not exist is a line that carries air, and the cost of that air is paid on every parcel.
There is also a throughput cost to width that is easy to miss. A wider belt at the same speed moves the same number of segments per hour, but each segment holds a larger parcel, which changes the induction pattern and often reduces the achievable density.
And there is a divert cost. A wider belt needs a longer push stroke, which needs more time or more force, which changes the divert technology. The step from a narrow span to a wide one is sometimes a step from a simple pusher to a more complex mechanism.
The right width is the smallest span that carries the target share of the catalogue with an acceptable exception rate. Wider than that is capacity that will never be used, and the money belongs in the induction, the chutes or the exception lane.
The upgrade path should be designed before it is needed
A catalogue grows in the direction of its best selling categories. If those categories are near the width limit, the line will be undersized within a couple of seasons, and the retrofit will happen during peak rather than between peaks.
The cheapest upgrade path is modular length rather than width. Adding segments to a line costs frame and controls; widening it costs a new frame, new guards, new divert and a new chute set. A line designed for length extension is a line that can grow.
The second cheapest path is an exception lane that can be upgraded to a second sorter. A manual lane that is already sited, staffed and measured is a lane that can be replaced by a machine when the volume justifies it, without relocating anything.
What should be avoided is the assumption that the line can be widened later. It usually cannot, and a specification that leaves width as a future decision is a specification that has deferred the most expensive decision to the worst possible moment.
Write down the excluded categories
Every width decision excludes something, and the excluded list is the most useful document the project produces. It names the categories that will go to the manual lane, the volume they represent, and the labour that implies.
The list should be built from the category census rather than from a general description, and it should carry volumes rather than names. A list of five categories is a description. A list of five categories with their shares of daily parcels is a plan.
It should also carry the growth assumption. A category that is excluded today and growing at a meaningful rate is a category that will force a decision within the planning horizon, and knowing that in advance changes how much modularity is worth buying.
The final row of the list is the review trigger: the volume share at which the exclusion becomes unacceptable. That number converts the excluded list from a record into a management instrument, and it is the number that will be cited when the second line is proposed.
The machine this census points at is the narrow belt sorter with the three hundred millimetre span, and the extra span is bought for the categories it admits rather than for the parcels it already carries.
- Build the width decision from a category census rather than a dimension average.
- Measure the packed width of each category, not the catalogue width.
- State the primary and exception operating modes with separate throughputs.
- Do not quote dual lane throughput as the design figure.
- Standardise parcel orientation at induction with a gate or a written rule.
- Measure the mix in soft and rigid groups rather than as one average.
- Select centring against the observed spread of induction positions.
- Size chute openings from the parcel, not from the belt width.
- Compare the wider span on cost per parcel against manual lane labour.
- Prefer modular length over width as the upgrade path.
- Record the excluded categories with their daily volume shares.
- Set a review trigger volume at which the exclusion becomes unacceptable.