A belt width is a promise about the widest parcel you will ever accept
Belt width is quoted as a single number and behaves like a set of three. It fixes the largest rectangle a parcel can occupy, the smallest gap a parcel can fall through, and the amount of lateral drift the line will forgive before a parcel touches a guard.
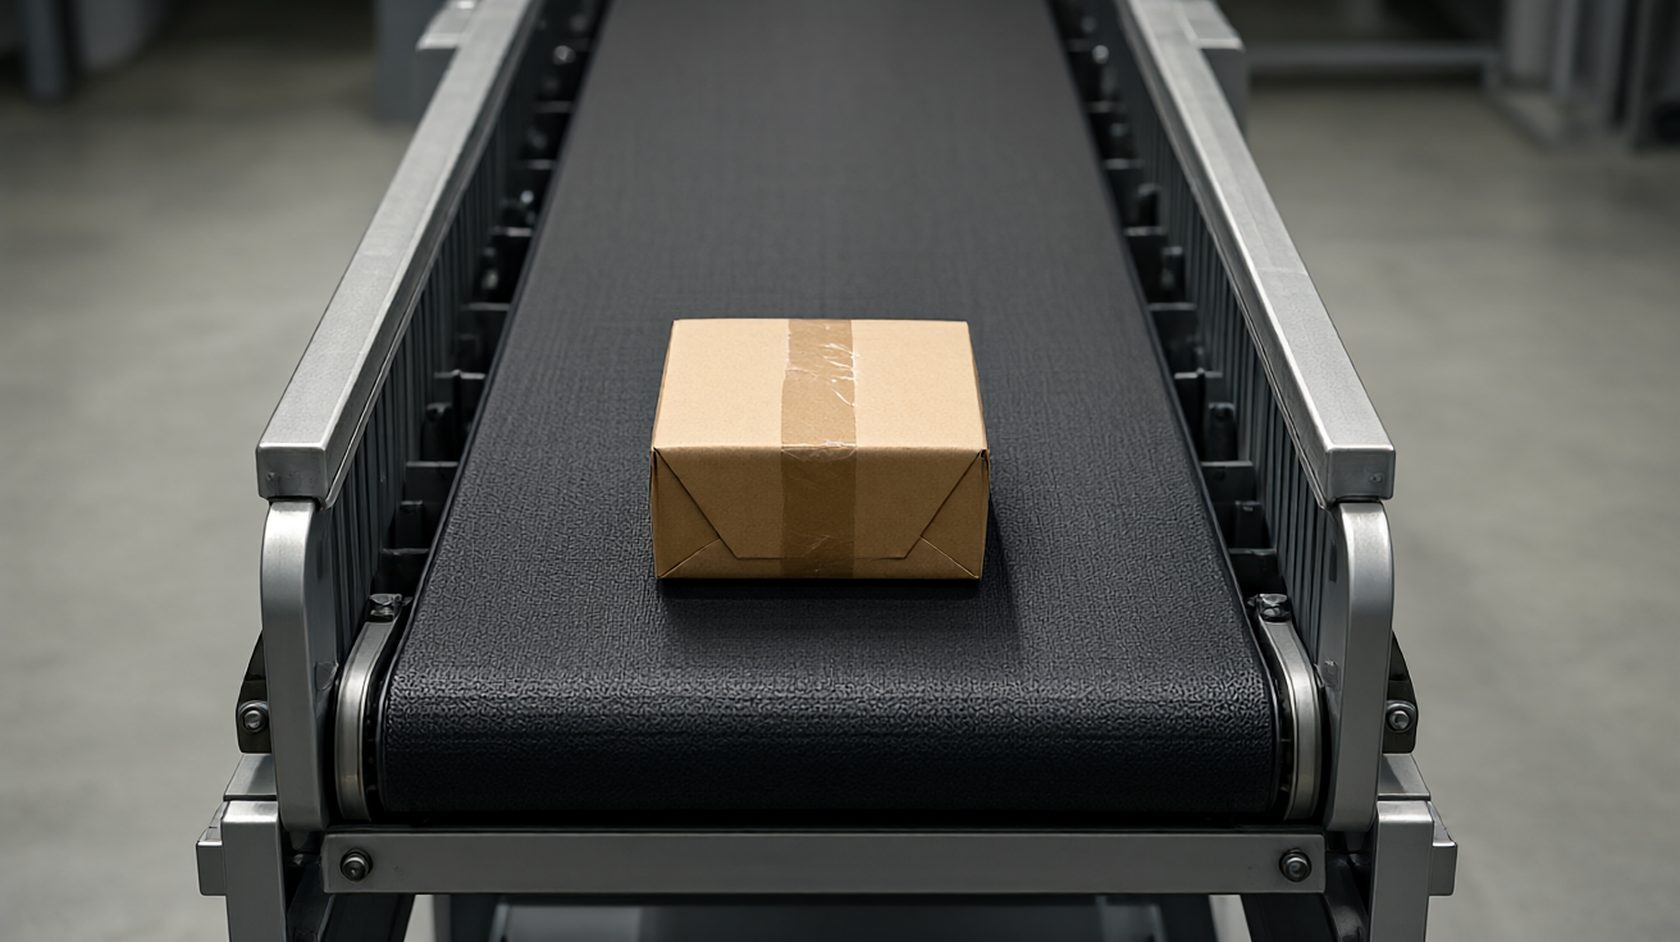
The envelope is a rectangle and the parcel is not
A sorter is specified against a rectangular envelope: maximum length, maximum width, maximum height. Parcels are not rectangular. A padded mailer is wider at one end, a boxed item bulges at the seam, and a bag settles into whatever shape the belt gives it. The envelope is therefore a test that a parcel either passes or fails at the point of induction.
This is why the usable width is not the nominal width. A belt quoted at two hundred millimetres has guards, a centring device and a frame on either side, and the parcel has to fit inside the clear span rather than inside the nominal figure. The difference is usually the first thing a buyer discovers after the line is installed.
The practical consequence is that the width should be specified from the parcel mix rather than from the catalogue. Take the ninety fifth percentile of parcel width by volume, add the bulge that packaging introduces, and check whether the resulting number sits comfortably inside the clear span.
The ninety fifth percentile rather than the maximum is a deliberate choice. Designing for the single widest parcel in a year means paying for width on every parcel for the rest of the year, and the widest parcel can usually be routed to a different line or handled manually.
Width sets the diagonal, not the length
A parcel that is too wide can sometimes be placed diagonally, and this is the reasoning that gets buyers into trouble. The diagonal of a rectangle is longer than either side, so a parcel wider than the belt can physically sit on it if it is rotated. What the diagonal does not account for is what happens next.
A rotated parcel occupies more of the belt's length than its narrow dimension suggests. On a short pitch line that means it occupies two segments instead of one, which halves the effective throughput for that parcel and creates a gap behind it that the induction logic has to fill.
The rotated parcel also drifts. Any lateral force, a centring wheel, a divert, or a slight camber in the frame, pushes a diagonally placed parcel toward one guard, and the guard is where the parcel either rubs or jams. The diagonal trick works on a short gravity conveyor and fails on a powered line.
The correct treatment is to treat the diagonal as unavailable for design capacity and available only as an exception path. If the operation expects a meaningful share of oversize parcels, the answer is a wider belt or a separate line, not a rotation rule at induction.
Where two hundred millimetres stops
A two hundred millimetre clear span carries the flat and the small: documents, padded mailers, single phone boxes, cosmetics, and a shoe box laid on its side. It is a genuinely useful width for a parcel mix that is dominated by small e commerce items, which is the mix most operations actually have.
What it does not carry is a shoe box standing on its base, a small appliance carton, or anything shipped in a retail box that was designed for a shelf rather than for a belt. Those are not marginal cases, they are the top of the width distribution, and they arrive every day rather than occasionally.
The failure mode is not a clean rejection. A parcel that is slightly too wide will sit on the belt with its edges overhanging the guards, which reads as acceptable until the parcel reaches a divert or a curve. At that point the overhang catches, the parcel rotates, and the jam takes a line stop to clear.
Which means the decision at two hundred millimetres is a decision about how much of the catalogue is excluded. If the answer is a small tail, the tail can be routed elsewhere. If the answer is the second largest category by volume, the width is wrong and the line will run below its rated capacity permanently.
What the next step up buys
The next standard step buys the retail carton. It carries the shoe box upright, the small appliance, the boxed toy, and it allows two narrow parcels side by side when the induction logic is willing to place them. Those three capabilities are the entire commercial case for the wider belt.
The cost is not only the belt. Wider means a wider frame, wider guards, a larger divert mechanism, a bigger footprint, and a centring device sized for the larger span. The increment is usually proportional rather than additive, which is why the step from the narrowest to the next one is often the most expensive single decision in the line.
Side by side placement is the capability that buyers overestimate. Two parcels travelling abreast need both to be within the same segment and both to be destined for chutes that the divert can reach in the same pass. In practice the second condition fails often enough that the arrangement is used as an exception rather than a design assumption.
The honest test is to count the parcels in a week of real shipments that would fail on the narrow width and would pass on the wider one. If that count is under a couple of percent, the narrower belt with a manual exception lane is cheaper over the life of the line.
Rejection is a process, not an accident
An oversize parcel has to be identified at induction, before it reaches the belt. Identification at the first divert is identification too late, because by then the parcel is already occupying space on a line that has other parcels behind it.
The measurement point should be a dimensioner or a simple width gate at the infeed, and the outcome should be a routed rejection rather than a stop. A gate that stops the line for every oversize parcel converts a parcel problem into a throughput problem, and the operator learns to disable the gate.
The rejection lane needs a defined capacity and a defined owner. A lane that fills up over a shift and is cleared at the end of it is a lane that has absorbed the parcels the line could not take, and the labour to clear it is the real cost of the width decision.
The procedure should also state what happens to a parcel that passes the gate but jams later. That is a different failure with a different response, and conflating the two produces a rejection policy that does not match the actual failure distribution.
Centring matters more than another hundred millimetres
A parcel that sits off centre by fifty millimetres on a narrow belt is closer to a guard than a parcel that sits centred on a belt a hundred millimetres wider. Centring is therefore a cheaper intervention than widening, and it addresses the failure that widening is usually bought to solve.
Centring devices are mechanical, pneumatic or a pair of angled rollers, and each has a parcel mix it handles badly. A device tuned for rigid cartons will fold a padded mailer, and a device tuned for mailers will fail to move a heavy carton. The device has to be selected against the mix, not against the average.
The measurement that decides whether centring is working is the distribution of parcel positions at the divert, not at the infeed. A parcel that enters centred and drifts by the time it reaches the divert is a tracking problem, and no amount of centring at the infeed will fix it.
Where the mix is genuinely bimodal, rigid cartons and soft mailers in similar volumes, two induction lanes with different centring devices is often cheaper than one lane wide enough to forgive both. The lanes cost floor space and they remove the compromise.
The smallest parcel is the other end of the envelope
Every discussion of belt width is a discussion of the maximum, and the minimum is where the line quietly fails. A parcel smaller than the gap between the belt and the guard will drop into it, and a parcel thin enough to fit between two rollers will orient itself into the gap.
The minimum is set by the clear gap at the edges and by the transition points between conveyor sections. Transitions are the worst case, because the gap between two sections is wider than the gap along either of them, and a small flat parcel will find it.
The answer is usually a plate or a small item kit rather than a narrower belt. A transition plate covers the gap, a raised guard closes the edge, and both are cheaper than re specifiying the line. The cost is that the plate introduces a step that a very flat parcel can catch on.
Which means the small item problem has a floor. Below a certain thickness and weight, a belt sorter is the wrong machine and the answer is a chute sorter or manual handling. Recognising that floor during specification is much cheaper than discovering it during commissioning.
Tension and tracking on a narrow belt
A narrow belt is less forgiving of tension imbalance than a wide one. The same absolute tracking error is a larger fraction of the belt width, so the belt reaches the guard sooner, and a belt that runs against a guard wears its edge and then fails.
The tensioning arrangement has to allow adjustment on both sides independently, because a single central tensioner cannot correct a belt that is tracking to one side. On a wide belt the error is absorbed by the width; on a narrow belt it is not.
Belt material matters for the same reason. A belt with a fabric carcass stretches unevenly under load, and on a narrow belt the unevenness shows up as tracking drift within a shift rather than seasonally. A belt with a more dimensionally stable carcass costs more and tracks better.
The maintenance implication is that tracking has to be checked on a schedule rather than on a complaint. A weekly check that takes a minute per belt prevents the edge wear that turns into a belt replacement, and belt replacement on a narrow line is a downtime event rather than a maintenance task.
Throughput does not scale with width
Wider belts are often bought with an implied throughput increase, and the increase does not arrive unless the constraint was parcel width. If the line is limited by pitch, speed or induction rate, a wider belt moves the same number of parcels per hour and costs more to run.
The one case where width genuinely raises throughput is dual lane operation, where two parcels travel abreast in the same segment. That requires the induction logic, the divert reach and the chute spacing to all support it, and it is a system change rather than a belt change.
The other case is a mix where a significant share of parcels currently has to be rotated or spaced out because of width. Widening removes the rotation and the extra spacing, which recovers capacity without changing speed. This is the case worth paying for, and it should be quantified before the purchase.
The way to test it is to measure the share of parcels that consume more than one pitch because of width. If that share is low, the width is not the constraint and the money belongs somewhere else in the line.
The three rows to fill before signing
The first row is the largest parcel by each dimension, taken from actual shipment data rather than from the product catalogue. The catalogue describes what was sold; the shipment data describes what was packed, and the packed dimension is always larger.
The second row is the smallest parcel, measured the same way, with its thickness as well as its footprint. The thickness is what decides whether it falls into a gap, and it is the dimension that parcel data usually omits.
The third row is the share of daily volume that fails the candidate width. That number converts the width decision from a specification argument into a cost, because the share that fails is the share that has to be handled by an exception lane with its own labour.
With those three rows the decision is arithmetic rather than preference. The narrower belt with an exception lane and the wider belt without one can be compared on total cost per parcel, and the comparison will usually favour different answers for different catalogues, which is the point.
The configuration this note is built around is the narrow belt sorter sized for a two hundred millimetre span, and the clear span between its guards is the number that decides which parcels it will ever accept.
- Specify the clear span between guards rather than the nominal belt width.
- Take the ninety fifth percentile of packed width, not the catalogue width.
- Treat diagonal placement as an exception path, never as design capacity.
- Count the parcels per week that fail each candidate width before choosing.
- Put the measurement gate at induction, not at the first divert.
- Give the rejection lane a capacity and an owner.
- Measure parcel position at the divert, not only at the infeed.
- Close the small item gap with a transition plate rather than a narrower belt.
- Provide independent tension adjustment on both belt edges.
- Check tracking on a weekly schedule rather than on complaint.
- Quantify the share of parcels consuming extra pitch because of width.
- Compare total cost per parcel including the exception lane labour.